Global packaging manufacturer improves efficiency and reduces downtime with industrial IoT | Velotic

Global packaging manufacturer improves efficiency and reduces downtime with industrial IoT

A leading packaging company leveraged Kepware to secure OT networks and unify data across all facilities—without replacing legacy equipment.

Case study

Overview

50%
Reduction in daily and weekly production meeting time
16%
Improvement in overall equipment effectiveness (OEE)
Background

Background

See how a global packaging manufacturer used real-time monitoring, advanced analytics, and predictive maintenance capabilities to improve customer efficiency, reduce downtime, and create new service offerings.

A global packaging manufacturer delivers automated processing and packaging machines, services, and solutions to customers across industries including pharmaceuticals, cosmetics, food, tea, and coffee. With more than 6,200 employees, 46 manufacturing sites, and a network spanning 80 countries, the company has a long history of using new technologies to create value for its customers.

In 2016, the manufacturer established a dedicated digital organization to identify and implement new opportunities across its ecosystem. The effort began with 18 digital transformation projects and quickly expanded to 25 initiatives spanning customer services, internal processes, and products. These projects focused on areas including predictive maintenance and remote assistance.

Recognizing the potential value locked in production data, the company set out to build a customer-facing application that could deliver data-driven insights, improve efficiency, and transform its service offerings.

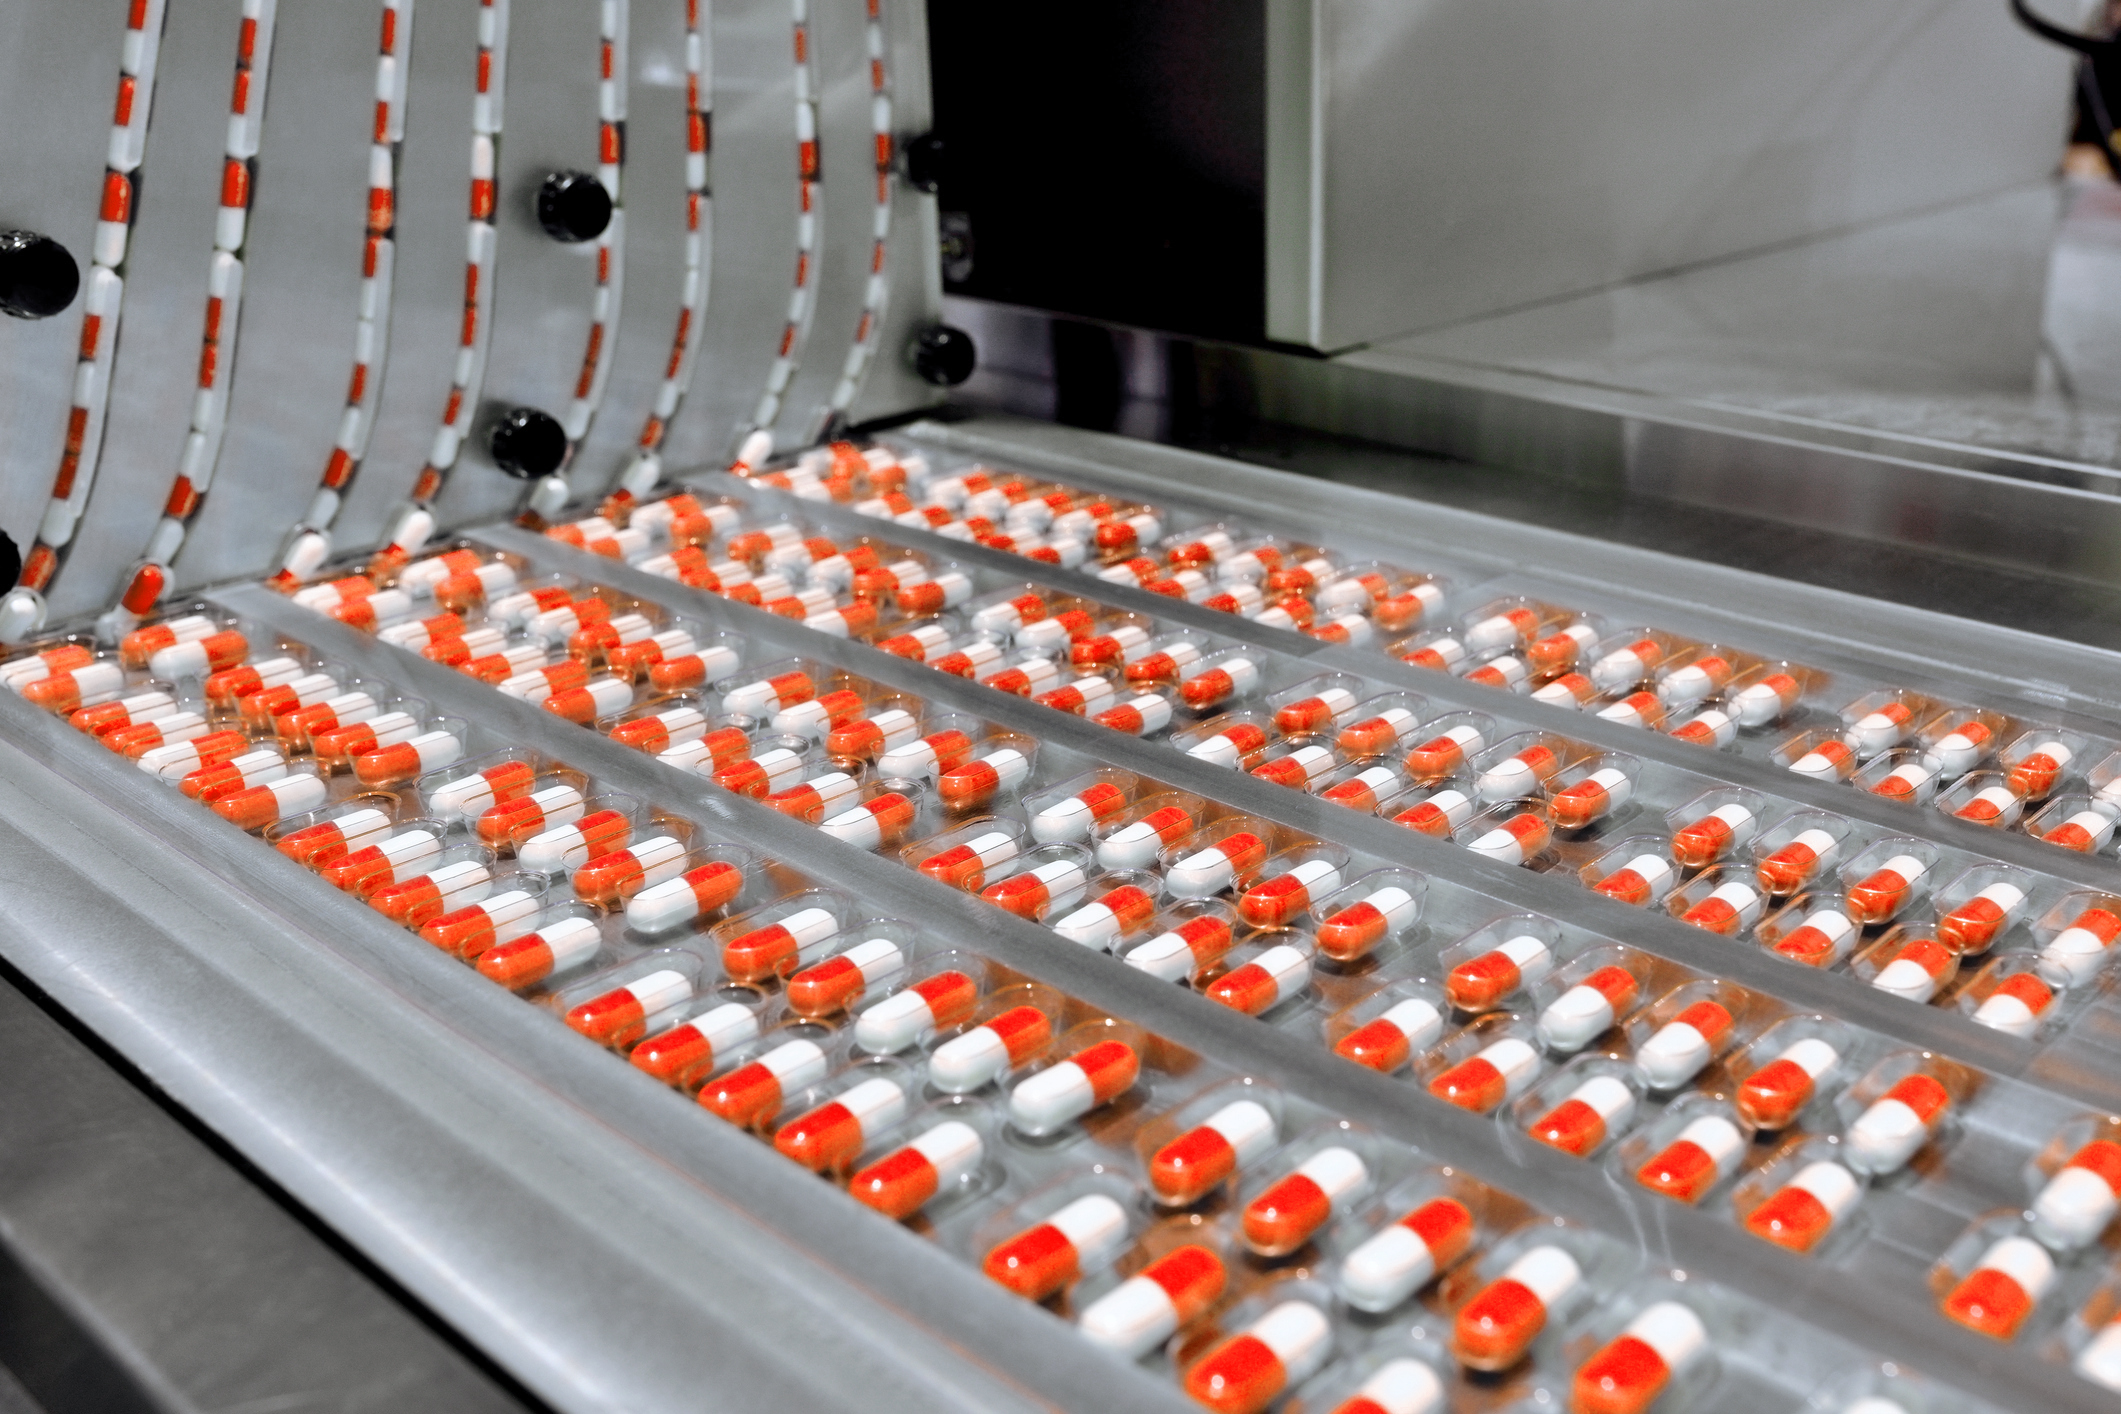
pharmaceutical packaging
The challenge

The challenge

Unlocking the power of production data

The global packaging manufacturer recognized that better access to production insights could help customers improve efficiency. Customers needed greater visibility into their operations to understand where inefficiencies originated, identify the causes of downtime, and make more informed decisions about production performance.

At the same time, the company wanted to expand beyond traditional services such as spare parts and technical assistance. Its goal was to move from product-centric support to more advanced, customer-centric services that could:

  • Improve overall equipment effectiveness
  • Reduce production downtime
  • Strengthen customer partnerships
  • Differentiate its service offerings
  • Create new revenue streams

Achieving that vision required the ability to connect a wide variety of new and legacy machines and PLCs built at different times with different technologies. The solution also needed to support equipment across customers’ entire production lines, including machines not produced by the global packaging manufacturer.

The growing need for remote collaboration and services added further urgency. When travel and access to customer sites became restricted during the COVID-19 pandemic, remote monitoring, troubleshooting, and support became essential to the company’s digital strategy.

The solution

The solution

Connecting machines and turning data into actionable insight

The global packaging manufacturer selected ThingWorx as the industrial IoT platform for its customer-facing solution, with Kepware Server providing industrial connectivity. Together, the technologies enabled the company to connect, collect, and analyze data across assets while supporting machine monitoring and automation use cases.

Kepware Server provided the flexibility to connect diverse legacy machines and PLCs, helping the manufacturer bring older equipment into a connected environment. This universal connectivity allowed customers to connect entire production lines, including equipment from other manufacturers. Its security capabilities provided a unidirectional network from the machine PLC to ThingWorx, blocking external requests or interactions with machine data.

The manufacturer deployed ThingWorx and Kepware Server in the cloud to simplify administration, support scalability, and provide a path for connecting additional assets and expanding storage as requirements grew.

Using ThingWorx, the company created a customer-facing application that monitors machine conditions in real time, collects raw production data, and translates it into useful information. A centralized dashboard gives operators access to operational data and insights that can support OEE improvements.

Key capabilities include: 

  • Intelligent, dynamic action lists that help operators improve efficiency
  • Machine data statistics that support line harmonization
  • Average performance information for production planning
  • Real-time analysis of efficiency losses and their sources
  • Recommendations that direct operators toward areas requiring attention
  • Benchmarking analysis across similar machines
  • Visibility into downtime events and their causes
  • Remote access to monitoring, troubleshooting, and insights across phones, tablets, and computers

The application communicates with ERP and MES systems and receives and analyzes data from PLCs, allowing it to use information from different types of machines across the production environment.

The manufacturer also introduced 24/7 control room services supported by experienced technicians. Customers receive detailed reports, specific alerts, and ongoing assistance. Support teams interpret machine data and algorithms to identify abnormal conditions, notify customers, and help them resolve problems. Longer-term reporting also helps customers identify trends and improve production performance over time.
manufacturing floor
The results

The results

Improving efficiency, reducing downtime, and expanding service value

The connected monitoring and analytics solution helped customers gain a more complete view of their systems and production processes. Real-time analysis allowed operators to identify the sources of efficiency losses, while benchmarking between similar machines provided greater insight into historical performance, downtime events, and their causes.

Documented results included: 

  • Up to 16% improvement in OEE in a specific customer success case
  • 50% less time spent in daily and weekly production meetings for some customers
  • Improved manufacturing efficiency through benchmark and loss analysis
  • Reduced downtime through greater visibility and awareness
  • Impoved production processes through increased employee engagement
  • Deeper employee understanding of production operations
  • Additional time savings for production personnel 

The initiative also helped the global packaging manufacturer evolve from traditional, product-centric services to advanced, customer-centric offerings. These new services strengthened customer relationships and created new revenue streams. Operational data from connected machines also established a feedback loop that gave the company a better understanding of how its products performed in the field.

Transform machine data into better service

Learn how Velotic helps industrial organizations connect equipment, monitor production remotely, and use operational insights to improve service response, reduce downtime, and support predictive maintenance.

Talk to an expert
What's next

What's next

IMA isn’t stopping there. They have their sights set on incorporating new features and technologies to build on the solutions they’ve created. Specifically, they want to raise the bar with artificial intelligence (AI) by improving on their anomalous and predictive algorithms. By applying analytics and AI to a variety of machines, IMA could disseminate services to more customers on a broader scale. 

Turn production insights into action

connect new and legacy assets, gain real-time operational visibility, and help teams improve efficiency with ThingWorx and Kepware Server.

Explore ThingWorx

Continue reading